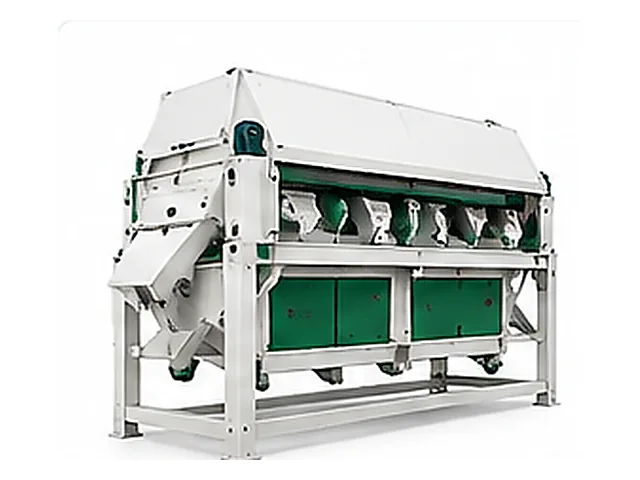
 Cleaning & Pre-Cleaning
Pre-Cleaner
Equipment for a defined process step; final setup depends on crop and target grade.
5–40 t/h↗
A barley processing line should be planned around the incoming sample and the final product specification. Key considerations include removing awns and straw fragments, controlling broken kernels, and grading barley to its malting, feed or food destination. These findings help determine whether pre-cleaning, aspiration, screening, density separation or optical sorting is appropriate. The final sequence and throughput should be confirmed using a representative sample and a written supplier offer.
Planning information only: capacity and configuration vary depending on the product and foreign-material profile.
Equipment for cleaning, grading, separation, optical sorting and handling.
Cleaning & Pre-CleaningEquipment for a defined process step; final setup depends on crop and target grade.
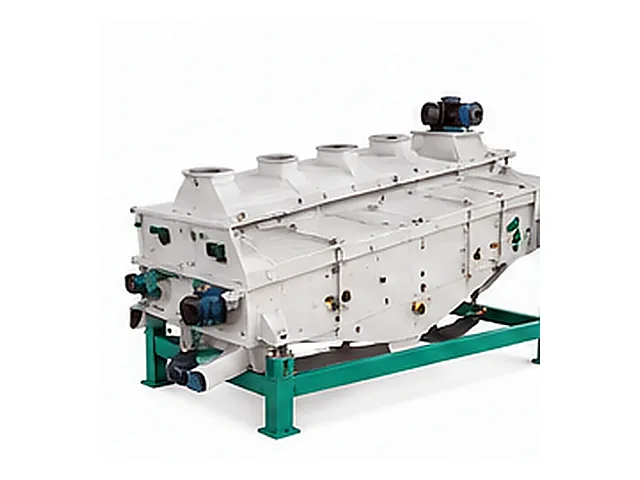 Cleaning & Pre-Cleaning
Equipment for a defined process step; final setup depends on crop and target grade.
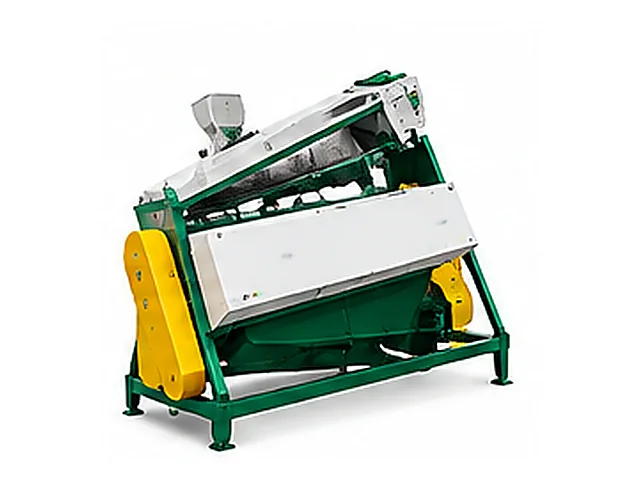 Separation
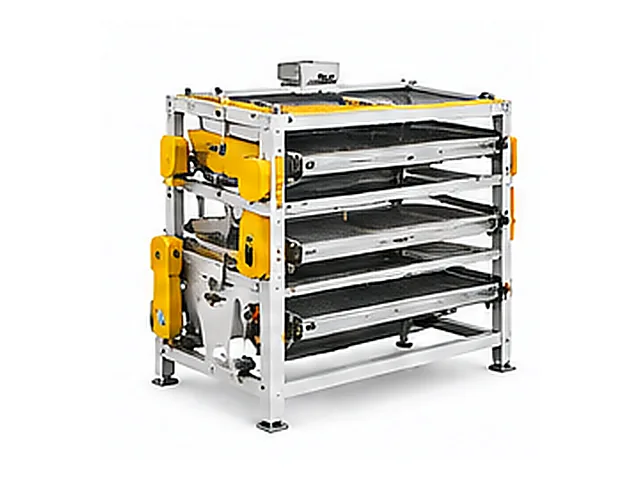 Grading & Sizing
Equipment for a defined process step; final setup depends on crop and target grade.
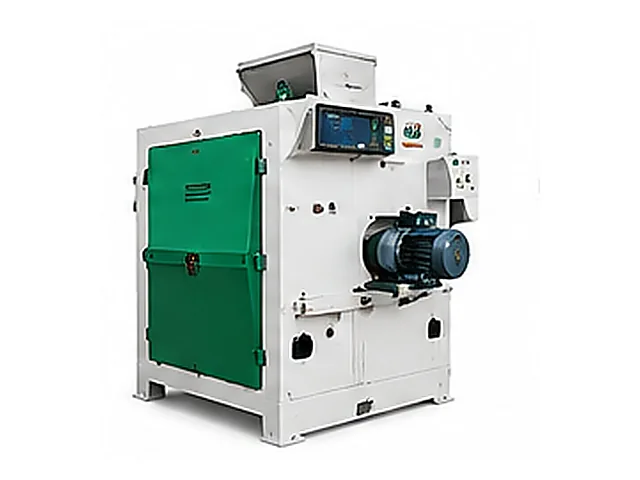 Separation
Equipment for a defined process step; final setup depends on crop and target grade.
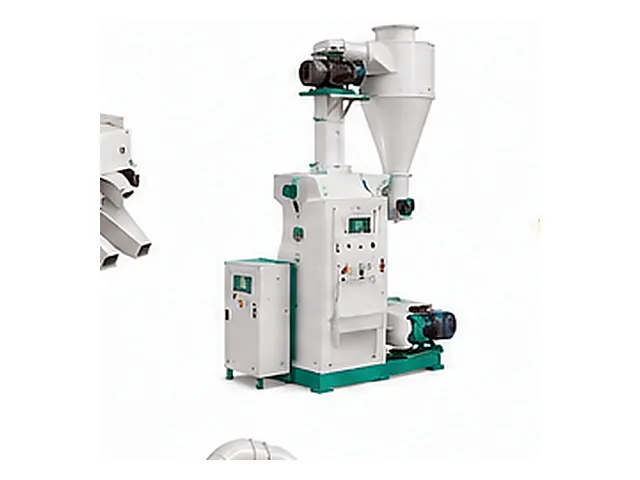 Cleaning & Pre-Cleaning
Equipment for a defined process step; final setup depends on crop and target grade.
 Conveying & Elevation
Equipment for a defined process step; final setup depends on crop and target grade.
A barley processing line should be planned around incoming material condition and the final product specification. Key considerations include removing awns and straw fragments, controlling broken kernels, and grading barley to its malting, feed or food destination. The objective is to remove unwanted material without unnecessary loss of saleable product.
Planning starts with receiving, sampling and defining acceptance criteria. Depending on the sample, the line may use pre-cleaning, aspiration, screen grading, destoning or density separation, and optional optical sorting. Not every crop requires every stage; the sequence should be verified against the sample and final specification.
A barley cleaning machine or other barley processing equipment should not be selected on capacity alone. Screen openings, airflow, feeding method, product-contact materials, access for cleaning and downstream connections all matter. Start by reviewing Pre-Cleaner, Air Screen Cleaning Machine, Destoner, then confirm the final configuration with the supplier using a representative sample and target grade.
Incoming moisture, impurity profile, variation in seed or kernel size, and the intended food, feed, oil, spice or seed-market destination all affect equipment selection. Aggressive handling can increase breakage or losses, while insufficient separation may miss the target purity. Cleaning efficiency and saleable-product recovery should therefore be assessed together.
For malting barley, kernel integrity and grade requirements should be defined before the equipment offer is compared.
When planning a barley processing plant or complete seed processing line, define capacity, product quality and acceptance criteria clearly to support an accurate project quotation. Confirm throughput, dimensions, utilities, accessories, installation, commissioning and warranty conditions in writing.
For barley processing, define the incoming product form, moisture condition where relevant, impurity profile, target purity and acceptable level of broken or defective material before selecting equipment. These details help determine not only the right machine, but also the sequence of equipment and inspection points across the line.
For malting barley, kernel integrity and grade requirements should be defined before the equipment offer is compared. For grains, the intended destination—flour, food, feed or seed—affects the cleaning sequence and the importance of kernel integrity. Cleaning efficiency should be reviewed alongside saleable-product recovery. Testing the same representative sample helps establish realistic expectations for target purity, product losses and the adjustment range required.
When comparing quotations, document throughput assumptions, product-contact materials, dust extraction, access for maintenance and cleaning, conveying interfaces and the next packaging or processing step. Ask the supplier to confirm operating conditions and capacity using a representative sample.
Inspect an incoming sample for stones, dust, husks, stems and other foreign material. The impurity profile can vary with harvesting and storage conditions.
Pre-cleaning removes coarse and light material, while fine cleaning targets smaller particles. Screen and airflow settings should be selected using a representative sample.
That depends on kernel size, shape, density differences and the target quality. Sample testing helps identify useful separation stages and estimate product loss.
Throughput planning considers moisture, impurity level, kernel characteristics, target purity and operating hours.
Check moisture, residual impurities, product integrity and the required quality. Storage conditions should suit the crop and its intended use.